News
In CNC machining, the choice between an End Milling Cutter and a Face Milling Cutter determines not only surface quality but also cycle time, tool life, and overall profitability. While both are rotary cutting tools, their application logic diverges fundamentally based on part geometry, machine capability, and production goals. This guide moves beyond textbook definitions to deliver actionable selection criteria, backed by performance data and real-shop scenarios.
For pockets, walls, slots, contours, and 3D features. Versatile but engagement-limited.
For broad flat surfaces, high material removal, and superior flatness on open faces.
The first decision is not which cutter is better — it is what kind of surface or feature the job requires. Geometry dictates the tool, not the other way around.


Before comparing performance, we must define what each tool is designed to do. The distinction is not merely about shape but about cutting mechanics and application scope.
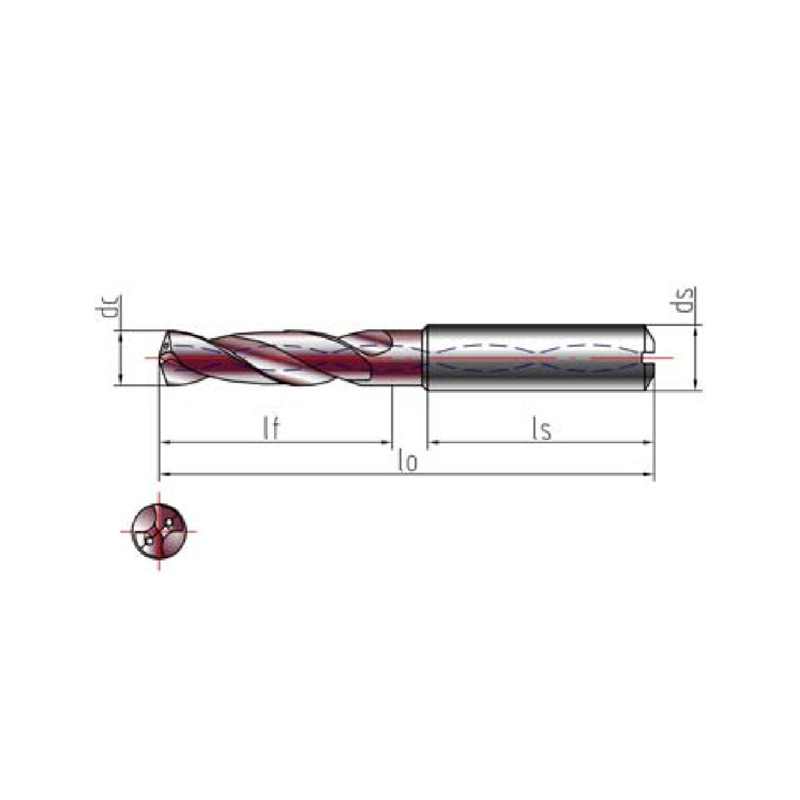
An Milling Cutter of the end variety cuts with both its periphery (sides) and its bottom face. This dual cutting capability allows it to perform slotting, profiling, pocketing, contouring, and even plunging operations. End mills are available in numerous configurations including square end, ball nose, and corner radius styles. Their smaller diameter and flute geometry enable access to confined features that larger tools cannot reach.
A face mill is designed primarily for cutting with its bottom face (the face of the cutter) to generate a flat surface on the workpiece. These tools are typically larger in diameter and feature multiple indexable inserts arranged around the body. Their primary advantage is surface coverage — each revolution sweeps a wide area, making them highly productive for surfacing large plates, squaring blocks, and preparing stock for subsequent operations.
The following comparison table summarizes the key differences based on six critical machining parameters.
Choosing between these tools requires analyzing five interrelated factors. Each influences not only initial selection but also downstream performance and cost.
This is the primary filter. If the tool must enter a pocket, follow a wall, or reach a confined area, an end mill is the only viable option. Face mills cannot machine internal features, complex contours, or non-planar surfaces. A square end mill is the default choice for most pocketing and slotting operations, while ball nose or corner radius variants handle contoured surfaces.
When the specification calls for a flat, broad surface with minimal waviness, a face mill with wiper inserts often produces superior flatness compared to an end mill stepping across the same area. However, a face mill can still produce a convex or non-flat surface if workholding distortion is present — a common issue in aluminum machining. Swapping cutters before checking fixturing can lead to wasted effort and expense.
For aluminum and other non-ferrous materials, face mills with PCD (polycrystalline diamond) inserts deliver excellent surface finish and tool life. For steel and cast iron, indexable carbide inserts with appropriate grades and coatings (such as TiAlN or AlTiN) are the norm. Solid carbide end mills, particularly those with AlTiN coatings, perform well in steel roughing and finishing, but are more susceptible to wear in high-heat conditions.
Face mills demand higher spindle torque and rigidity due to their larger diameter and higher cutting forces. A machine with inadequate rigidity will experience chatter, leading to poor surface finish and insert chipping. End mills, particularly smaller diameters, are more forgiving but may require higher spindle speeds to achieve optimal chip load and surface speed.
For small-batch or prototype work, end mills offer lower upfront cost and greater flexibility. For large-scale production with frequent surfacing operations, the per-part cost advantage of a face mill's high material removal rate often justifies the higher initial investment in indexable tooling.
The following charts present comparative performance data based on industry-standard benchmarks for end mills and face mills in typical steel machining applications. These figures are representative of medium-duty CNC milling operations.
Once the tool type is selected, the next step is parameter optimization. High-feed milling strategies differ significantly between end mills and face mills due to engagement mechanics.
This strategy uses a light radial engagement (5% to 15% of tool diameter) combined with a deep axial depth of cut (3x to 5x diameter). This distributes heat across the flute length, reduces thermal shock, and significantly extends tool life. Feed rates can be increased substantially because chip thinning is exploited. In steel, this approach can increase material removal rates by 30% to 40% compared to conventional roughing.
High-feed face mills are designed with a small entering angle, directing cutting forces primarily into the spindle. This allows for high feed rates (up to 1.5 mm/tooth in some materials) with moderate depths of cut (1-3 mm). The strategy excels in roughing and semi-finishing of large flat surfaces, achieving metal removal rates that end mills cannot match on broad faces.
Chip load is not interchangeable with feed rate. Feed rate (mm/min) = feed per tooth × number of flutes × RPM. Too low a chip load thins the chip, concentrating heat and accelerating wear. Too high a load causes deflection or breakage.
Tool selection is incomplete without considering the setup. The following workflow diagram illustrates the decision logic for selecting between end mills and face mills in a typical CNC milling environment.
Based on the analysis above, here is a structured decision framework that translates technical considerations into actionable choices.
Many parts benefit from a combination of both tools. A typical workflow might use a face mill for rough surfacing, followed by an end mill for finishing walls, pockets, and contours. This hybrid strategy leverages the strength of each tool while minimizing their weaknesses.
Yes, end mills can perform face milling tasks, particularly when the surface area is small or the geometry is complex. However, a dedicated face mill is more efficient for large flat surfaces due to its broader cutting diameter and higher metal removal rate.
A shell mill is a larger cutter that mounts on a separate arbor and is typically used on horizontal milling machines. A face mill is usually a self-contained tool with integral shank, more commonly used on vertical machining centers. Face mills have largely replaced shell mills for flat surface work in vertical CNC machines.
For aluminum, use end mills with polished flutes, high rake angles, and 2-3 flutes for efficient chip evacuation. For steel, use 4-5 flute end mills with AlTiN or TiAlN coatings to manage heat. For hardened materials (above 45 HRC), consider CBN or PCD tooling.
Radial engagement is the more aggressive variable for heat generation. A cutter with 100% radial engagement (full-width slotting) generates sustained, concentrated heat, reducing tool life. Light radial passes (5-15% of diameter) allow the tool to run cooler and last significantly longer.
This is often caused by workholding distortion (jaw lift, clamping stress) rather than the cutter itself. Check fixturing before assuming the face mill is the problem. In aluminum, this is a common issue that switching cutters will not resolve.

ChaiTools is specializing in the research and development, design, production, sales and technical support of high-end CNC tools.
 +86-571-83502022
 +86-18867120330
+86-18857186736
+86-13615816276
 +86-571-82529638
 11 Floor of No.2 Wanyushuzhigu Building, Dongrui 4# road, Xintang Street, Xiaoshan District, Hangzhou City, Zhejiang Province, China. POST CODE 311201
Copyright © 2022 Hangzhou Chai Cutting Tools Co., Ltd. All Rights Reserved. CNC Turning Tool Holders Manufacturers


 English
 Deutsch
 русский
 Español
 中文简体