News
In precision machining, selecting the appropriate tool for creating channels, recesses, or keyways is critical for maintaining dimensional accuracy and surface finish. While both the side and face milling cutter and the slot drill are employed for material removal, their mechanical designs and cutting actions differ significantly. A Groove Slot Milling Cutter refers to a category of tools optimized for deep or shallow linear paths, but the choice between a circular blade-style cutter and an end-cutting drill depends on the specific geometry of the workpiece.
The primary distinction lies in how the tool approaches the workpiece. A side and face cutter operates on an arbor and cuts primarily on its periphery and sides, whereas a slot drill is a shank-mounted tool that can plunge directly into the material. Understanding these mechanical nuances ensures higher efficiency and longer tool life in heavy-duty industrial environments.
Side and face cutters are disc-shaped tools with cutting teeth on the circumference and both flat sides. They are typically mounted on a horizontal milling machine arbor. This design allows the tool to maintain excellent rigidity during deep slotting operations, as the arbor provides support on both sides of the cutter, reducing deflection compared to cantilevered shank tools.
These cutters are the preferred choice for long, deep, or wide grooves where high metal removal rates are required. Because they have more teeth engaged in the cut simultaneously compared to a slot drill, they can handle higher feed rates and provide a more stable cutting action in tough materials like stainless steel or cast iron.
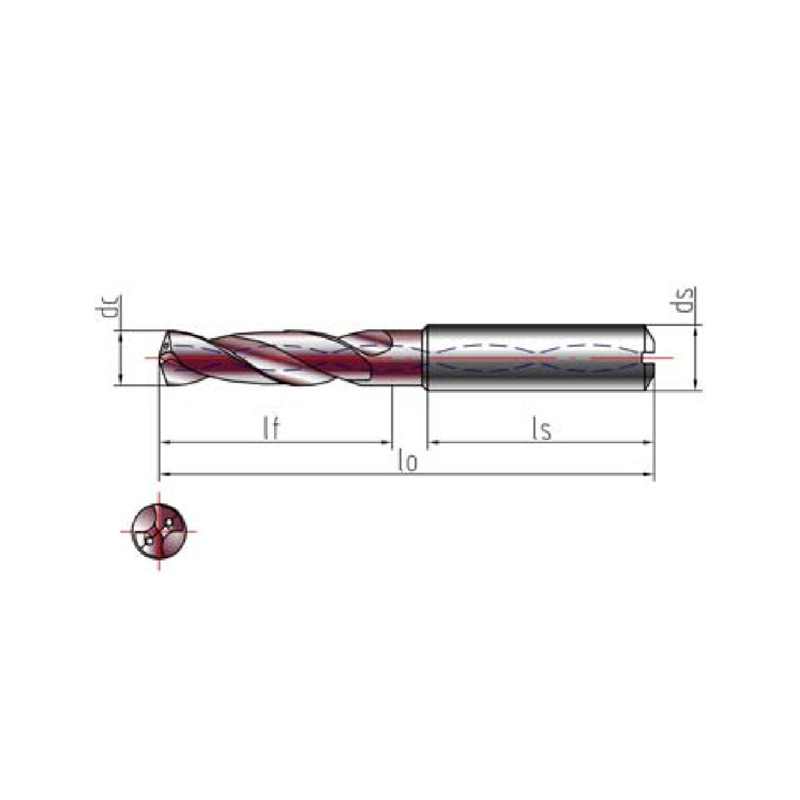
A slot drill is essentially a type of end mill, usually featuring two flutes. Unlike a standard four-flute end mill, the teeth of a slot drill meet at the center of the tool's end face. This allows the tool to plunge vertically into the workpiece like a drill bit before moving horizontally to create the slot. This dual-action capability makes it indispensable for blind slots or pockets where there is no entry point from the side of the material.
When machining keyways or closed slots, the slot drill offers unmatched versatility. However, because it is held by a shank in a collet or chuck, it is more susceptible to "tool walk" or deflection if excessive force is applied. Consequently, it is generally used for shallower slots or smaller diameter applications compared to large-scale disc cutters.
To choose the right Groove Slot Milling Cutter, engineers must evaluate the depth-to-width ratio and the accessibility of the slot. The following table summarizes the operational differences:
| Feature | Side and Face Cutter | Slot Drill |
| Mounting Method | Arbor Mounted | Shank Mounted (Collet) |
| Entry Method | Peripheral Entry Only | Plunge and Lateral |
| Ideal Slot Type | Open, Deep, Long | Closed, Blind, Short |
| Width Accuracy | High (Rigid Support) | Moderate (Deflection Risk) |
Use this tool when the project requires high-volume production of deep grooves. For instance, in the manufacturing of large industrial components where a slot depth of 50mm or more is required, the side and face cutter's ability to maintain verticality and width is superior. It is also the go-to for "straddle milling," where two cutters are used to machine two parallel surfaces simultaneously.
A slot drill is optimal for internal keyway cutting or CNC pocketing. If you are machining a housing for a bearing where the slot does not exit the side of the part, the slot drill is the only viable option. It is also more cost-effective for small-scale prototypes or one-off parts where complex arbor setups are not justified by the production volume.
To achieve the best results with a Groove Slot Milling Cutter, several parameters must be strictly controlled:
Yes, because its teeth meet at the center, it can plunge vertically. However, it is not optimized for deep hole drilling as it lacks the specialized flute geometry of a twist drill for long-range chip removal.
This is usually caused by tool deflection or "run-out" in the spindle. Using a high-precision collet and reducing the feed rate can help maintain the intended width.
Generally, a side and face milling cutter has a longer life in heavy production because it has more teeth to share the workload and its rigid mounting reduces vibration-induced wear.
No. Standard 4-flute end mills usually cannot plunge center-cut. You must drill a pilot hole first or use a ramp-in technique. Only 2-flute or specific "center-cutting" mills function as slot drills.

ChaiTools is specializing in the research and development, design, production, sales and technical support of high-end CNC tools.
 +86-571-83502022
 +86-18867120330
+86-18857186736
+86-13615816276
 +86-571-82529638
 11 Floor of No.2 Wanyushuzhigu Building, Dongrui 4# road, Xintang Street, Xiaoshan District, Hangzhou City, Zhejiang Province, China. POST CODE 311201
Copyright © 2022 Hangzhou Chai Cutting Tools Co., Ltd. All Rights Reserved. CNC Turning Tool Holders Manufacturers


 English
 Deutsch
 русский
 Español
 中文简体