News
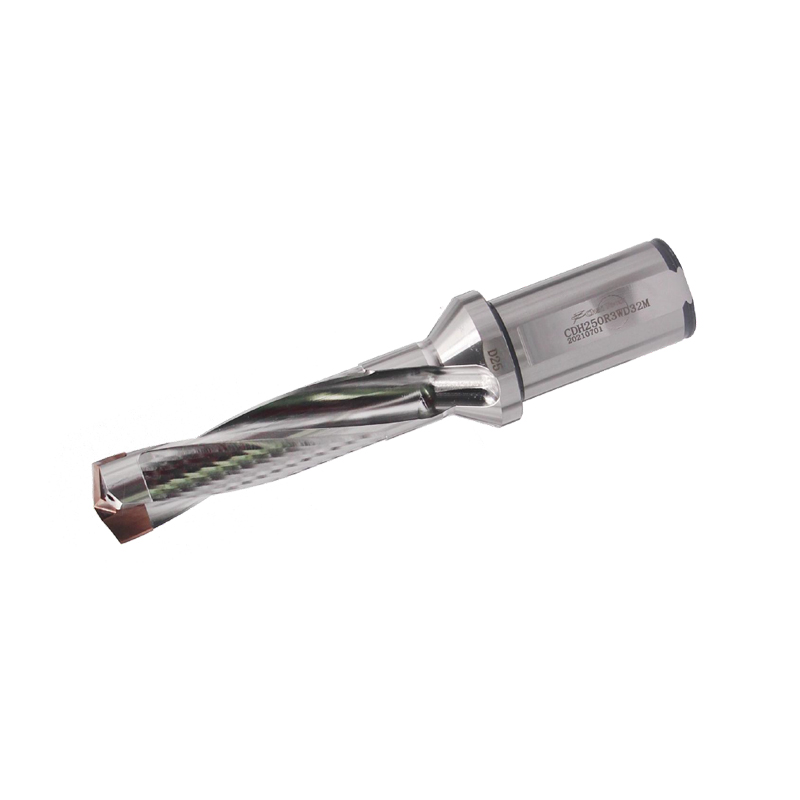
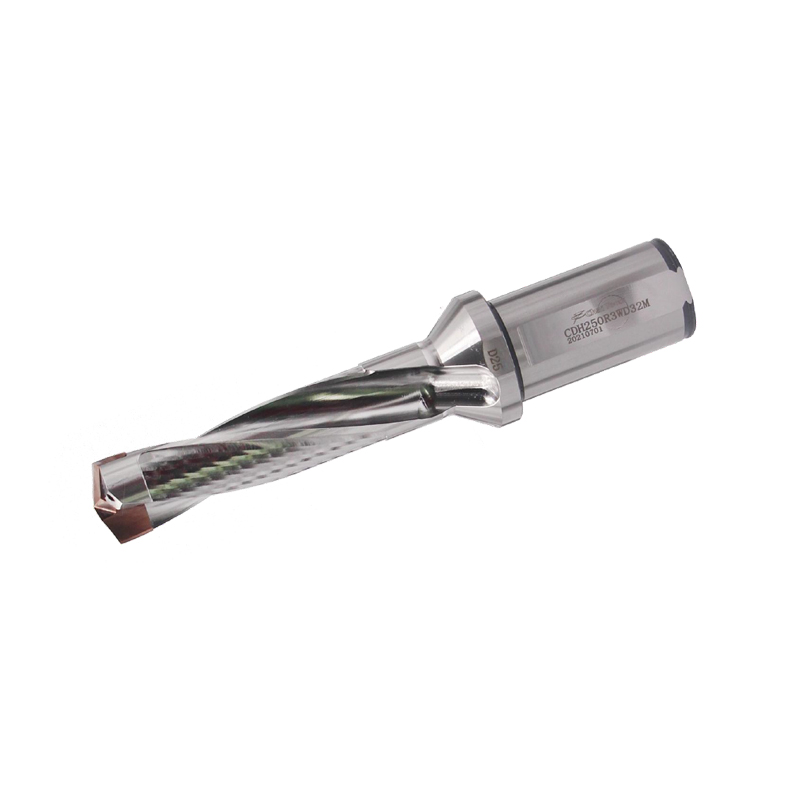
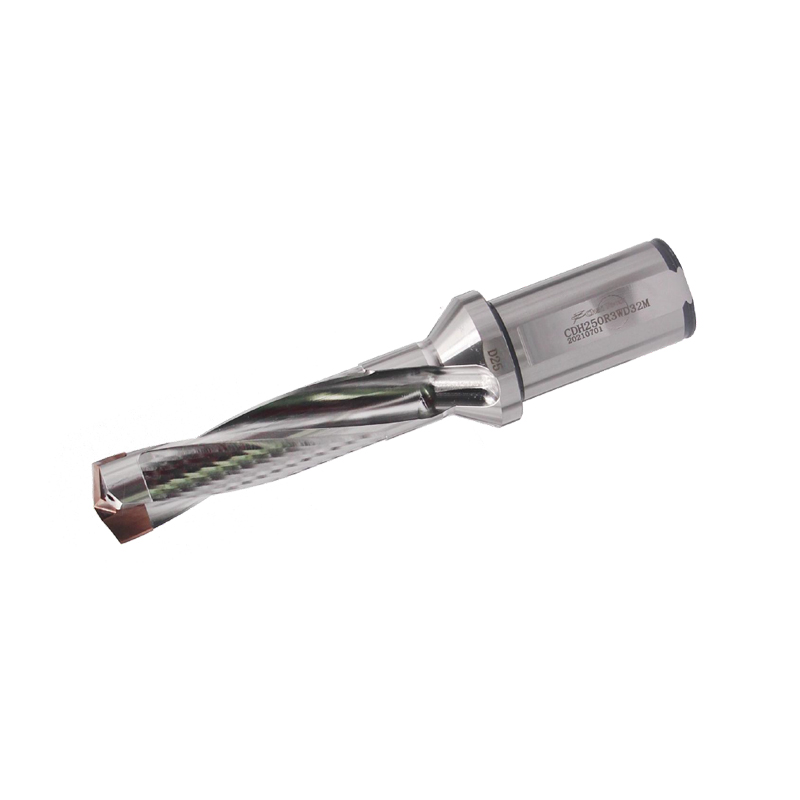
In the competitive landscape of industrial manufacturing, selecting the right cutting tool is not merely a technical choice but a financial one. While High-Speed Steel (HSS) has been a reliable staple for decades, the shift toward solid carbide drill technology has redefined the benchmarks for mass production. The fundamental difference lies in the micro-structure of the materials. Carbide is a composite material consisting of tungsten carbide particles sintered with a metallic binder, typically cobalt.
This composition results in a tool that is significantly harder and more wear-resistant than HSS. In mass production environments where machines run 24/7, the ability to maintain a sharp cutting edge under extreme heat is critical. HSS tools tend to soften at temperatures exceeding 500 degrees Celsius, whereas carbide maintains its structural integrity and hardness at much higher thermal thresholds. This thermal stability allows for significantly higher cutting speeds and feed rates.
To understand the superiority of carbide, one must analyze the physical properties that govern tool performance. Below is a comparative overview of how these materials behave under typical industrial loads.
| Property | HSS Tools | Solid Carbide Tools |
| Hardness (HRC) | 62 - 66 | 75 - 82 |
| Cutting Speed (m/min) | 20 - 40 | 80 - 150+ |
| Elastic Modulus (GPa) | ~210 | ~600 |
| Heat Resistance | Moderate | Excellent |
The Elastic Modulus of carbide is nearly three times that of steel. This means carbide drills are much stiffer, which directly translates to less deflection during the drilling process. In deep-hole applications or high-feed scenarios, this rigidity ensures that the hole remains straight and the diameter stays within tight tolerances.
In mass production, time is the most expensive variable. A reduction of even a few seconds in a drilling cycle can lead to massive cost savings when multiplied by thousands of units. Solid carbide allows for cutting speeds 3 to 5 times faster than HSS. For example, if a standard HSS drill requires 30 seconds to complete a hole in 4140 steel, a carbide equivalent might complete the same task in less than 8 seconds.
Carbide drills often feature advanced flute geometries and internal coolant holes that are difficult to manufacture in HSS. These features facilitate:
While the initial purchase price of carbide is higher than HSS, the total cost per hole is significantly lower in a production environment. The superior wear resistance of carbide means the tool can produce hundreds or even thousands more parts before requiring a tool change.
Consider the hidden costs of tool failure in an automated production line:
Statistically, in a high-volume automotive component run, transitioning to carbide can increase tool life by 10x to 20x compared to standard HSS drills, depending on the material hardness and coating used.
In B2B manufacturing, secondary operations like reaming or honing add unnecessary costs. Solid carbide drills produce a superior surface finish (lower Ra values) due to their rigidity and ability to withstand high surface footage. The lack of vibration and "walking" at the entry point ensures that the hole is concentric and properly positioned.
When dealing with materials like stainless steel, titanium, or hardened alloys (above 35 HRC), HSS often fails almost instantly. Carbide is the industry standard for these "difficult-to-machine" materials. The compressive strength of carbide allows it to penetrate hard surfaces without the edge crumbling, which is a frequent issue with brittle HSS variants at high temperatures.
To fully realize the benefits of carbide, the machining setup must be rigid. Unlike HSS, which can flex slightly to accommodate misalignment, carbide is brittle. Misalignment will lead to catastrophic tool breakage. Therefore, mass production facilities using carbide typically invest in:
For mass production and hard materials, yes. However, for manual hand drilling or unstable setups, HSS is preferred due to its toughness and flexibility.
Yes, they can be reground on specialized CNC grinding machines to restore their original geometry, extending their value.
The raw materials (Tungsten and Cobalt) are more expensive, and the manufacturing process involves complex sintering and diamond-wheel grinding.
Speeds vary by material, but generally, they should be 3 to 4 times higher than what is used for HSS in the same application.

ChaiTools is specializing in the research and development, design, production, sales and technical support of high-end CNC tools.
 +86-571-83502022
 +86-18867120330
+86-18857186736
+86-13615816276
 +86-571-82529638
 11 Floor of No.2 Wanyushuzhigu Building, Dongrui 4# road, Xintang Street, Xiaoshan District, Hangzhou City, Zhejiang Province, China. POST CODE 311201
Copyright © 2022 Hangzhou Chai Cutting Tools Co., Ltd. All Rights Reserved. CNC Turning Tool Holders Manufacturers


 English
 Deutsch
 русский
 Español
 中文简体